Category Archives: Uncategorized

GN Hydraulic Drive Centrifuges and Solids Control Equipment for Pakistan Deep Well Drilling Project

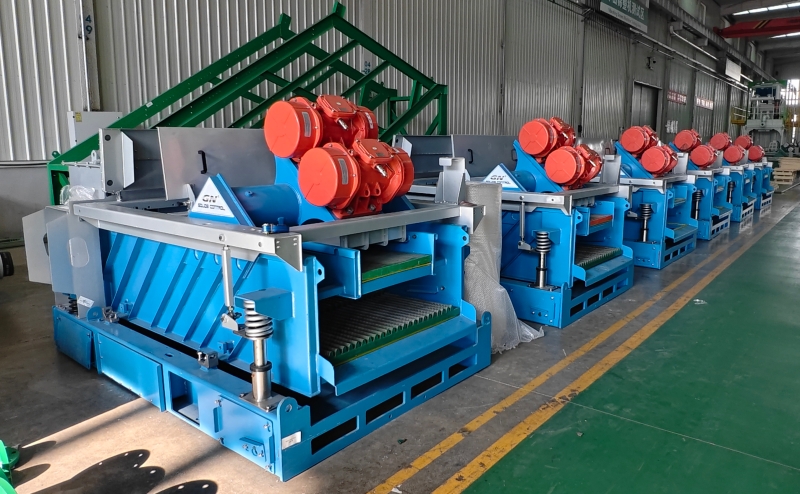
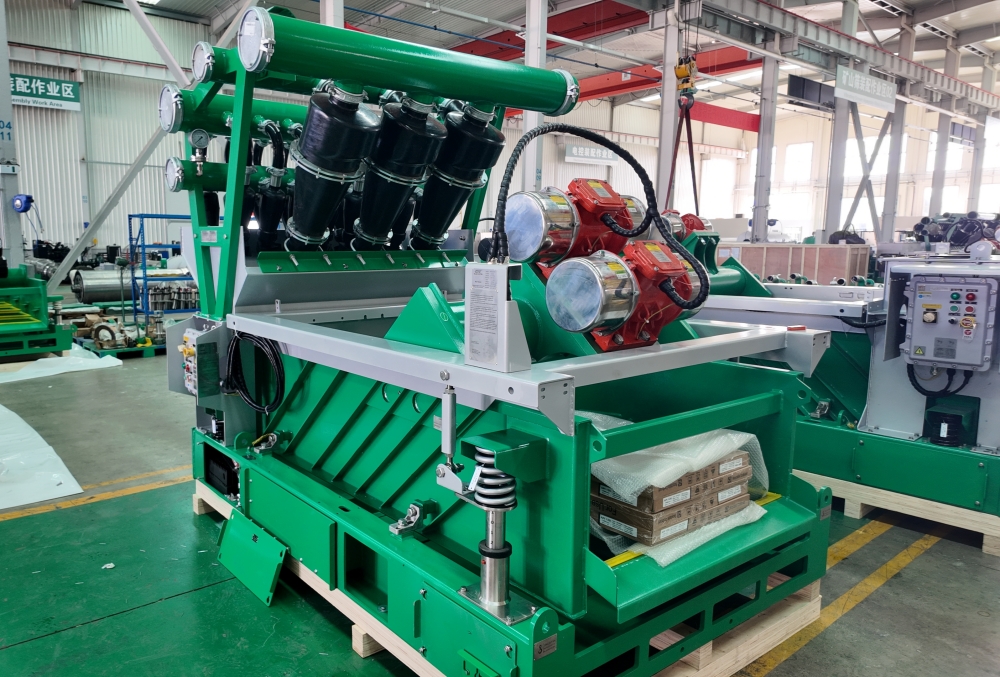
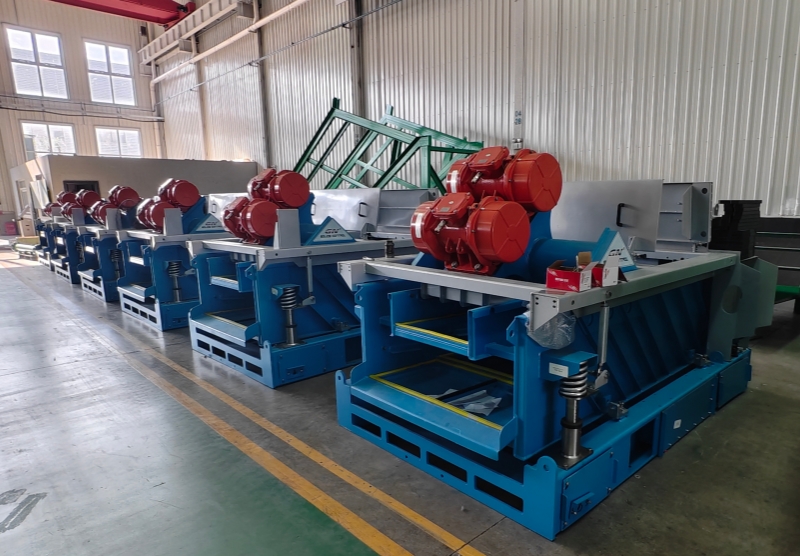
GN Solids Control is providing a package of solids control equipment for a deep well drilling project in Pakistan. The equipment package includes three GNZS595 drilling fluid shale shakers, one GNZJ594K-3S16N mud cleaner and two GNLW363D-FHD hydraulic drive decanter centrifuges. This integrated configuration is designed to support efficient drilling fluid treatment and solids removal throughout demanding deep well drilling operations.

Multi-Stage Solids Control Configuration
Effective drilling fluid management is essential for deep well drilling, where maintaining mud properties and controlling unwanted solids directly influence drilling performance and operational efficiency.
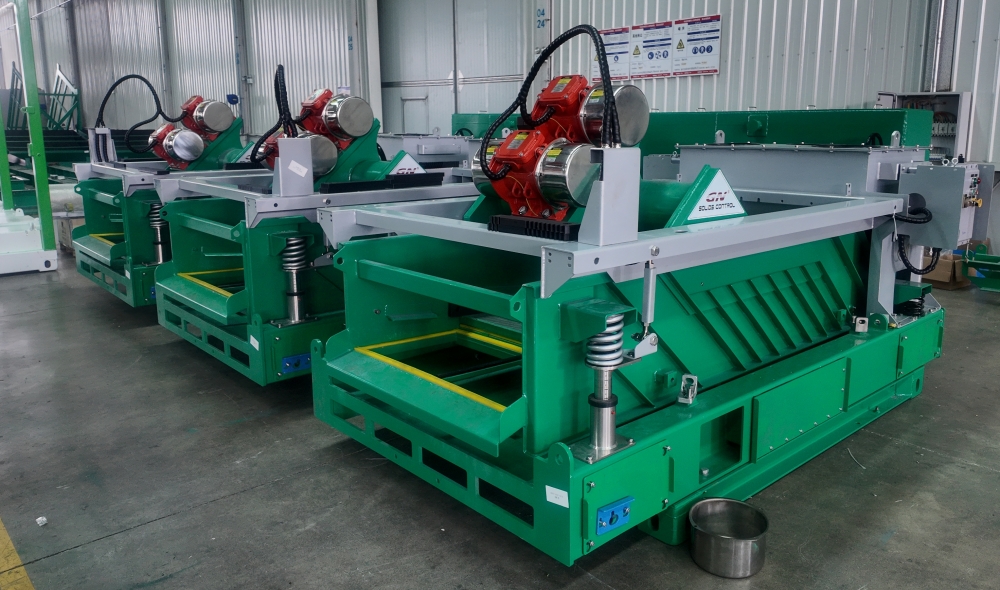
The three GNZS595 shale shakers serve as the primary solids separation equipment. By screening drilling fluid returning from the well, they remove larger drilled cuttings before the fluid proceeds to subsequent treatment stages.

Following primary separation, the GNZJ594K-3S16N mud cleaner provides additional solids removal through its integrated hydrocyclone and screening arrangement. This equipment helps separate finer solid particles that pass through the primary shale shakers, supporting improved drilling fluid cleanliness.

Hydraulic Drive Decanter Centrifuges
A key component of this project is the inclusion of two GNLW363D-FHD hydraulic drive decanter centrifuges.

Compared with conventional centrifuge drive configurations, hydraulic drive technology provides flexible differential speed adjustment, allowing operators to optimize centrifuge performance according to changing drilling fluid conditions.
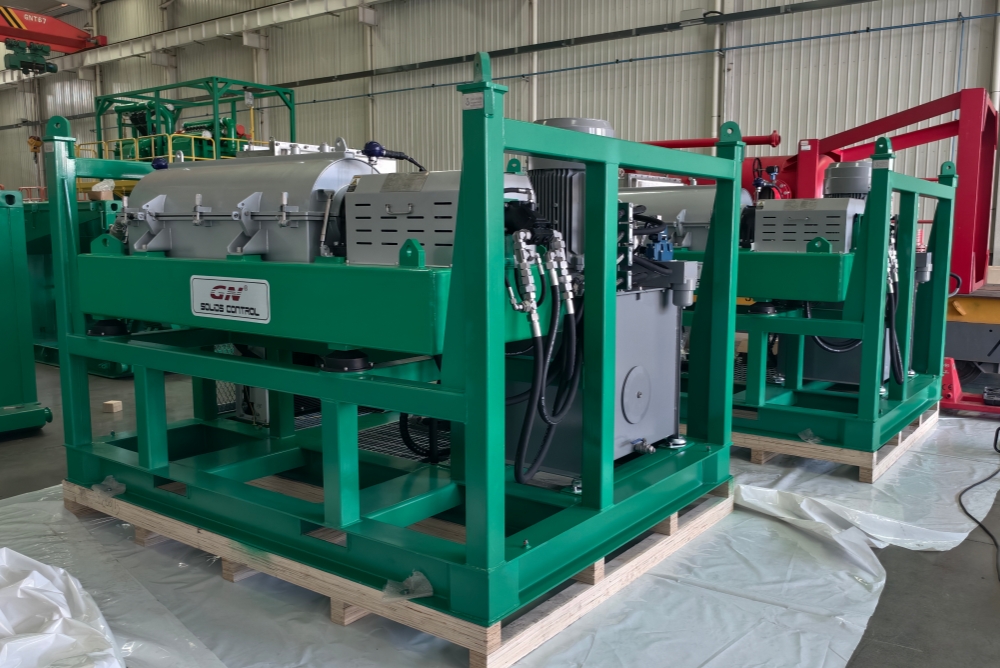
The hydraulic drive arrangement is particularly useful when processing drilling fluids with varying solids concentrations and particle characteristics. By adjusting the differential speed between the rotating bowl and screw conveyor, operators can achieve more flexible control over solids discharge and separation performance.

The GNLW363D-FHD centrifuges provide an additional fine-solids separation stage, helping remove smaller suspended particles that cannot be effectively eliminated by conventional screening and hydrocyclone equipment.

Supporting Efficient Deep Well Drilling
The combination of three shale shakers, one mud cleaner and two hydraulic drive centrifuges establishes a multi-stage solids control process, covering primary screening, hydrocyclone separation and centrifugal treatment.

This equipment configuration helps drilling contractors maintain drilling fluid quality, reduce unwanted solids accumulation and improve the potential for drilling fluid reuse. It also provides operational flexibility when dealing with different drilling conditions throughout the project.
GN Solids Control: Your Partner in Drilling Solutions
With extensive experience in solids control equipment manufacturing and engineering, GN Solids Control provides customized solutions for oil and gas drilling projects worldwide.

From individual shale shakers and mud cleaners to advanced hydraulic drive centrifuges and complete solids control systems, GN remains committed to delivering reliable equipment and professional technical support.

Through this Pakistan deep well drilling project, GN continues to demonstrate its capabilities in providing integrated drilling fluid processing solutions for challenging drilling applications.
GN Solids Control Presents at ADIPEC 2026 in Abu Dhabi

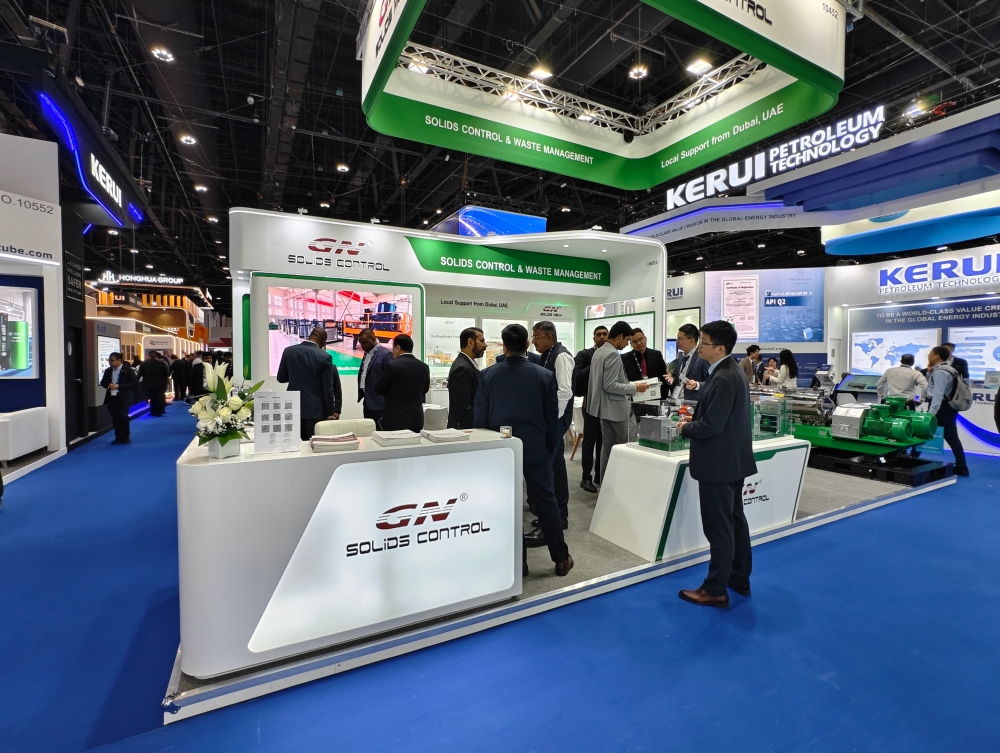
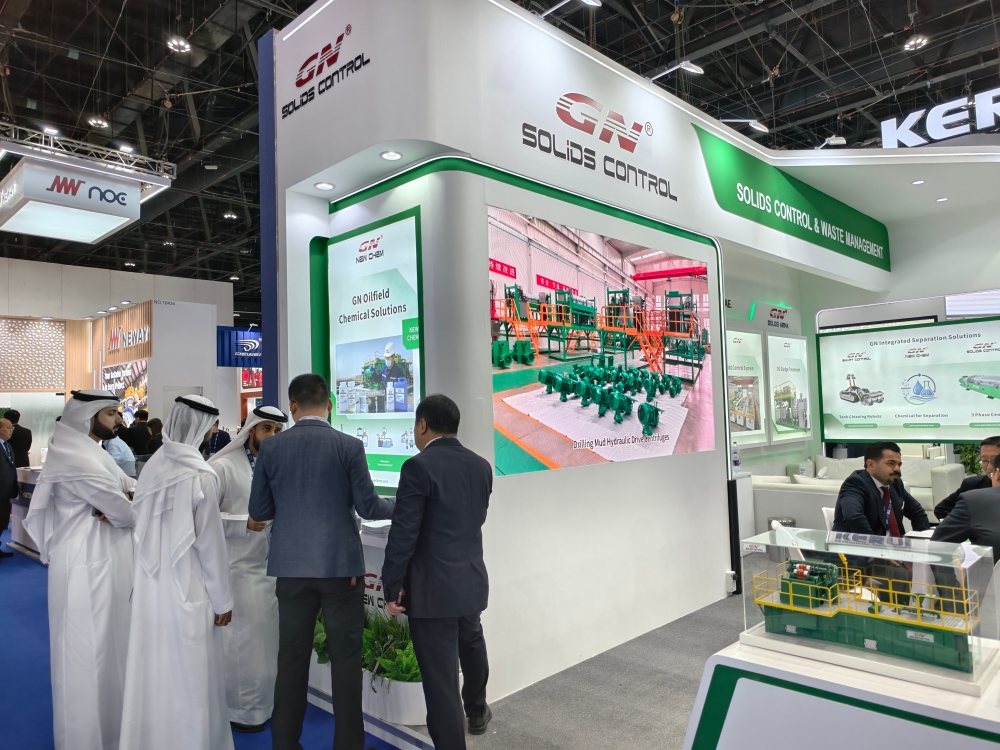
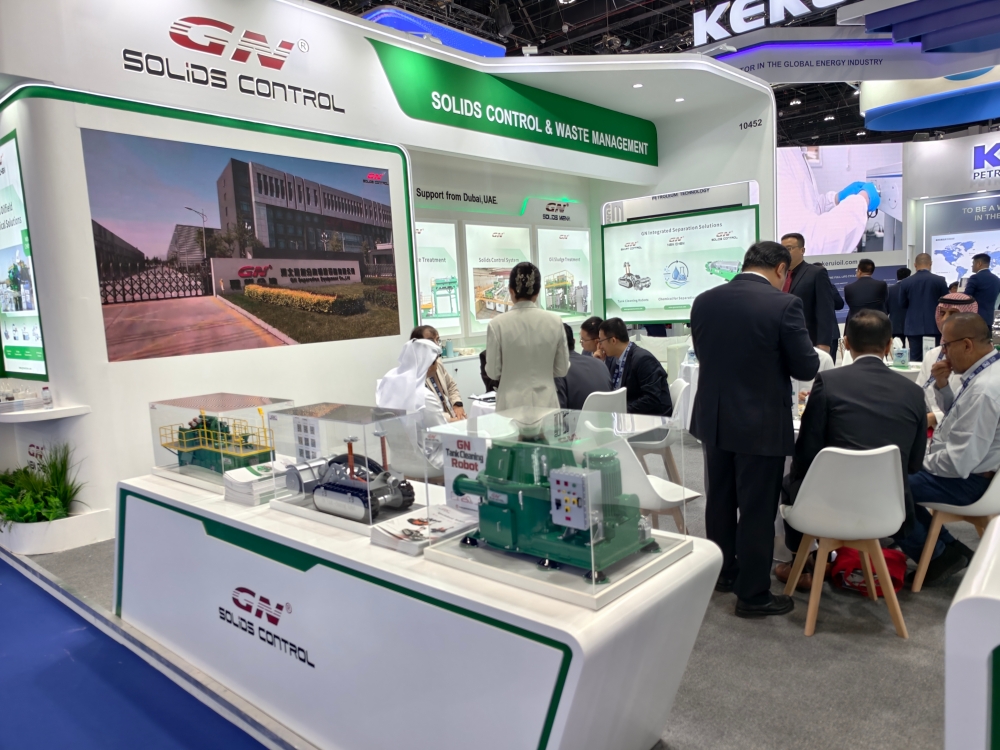
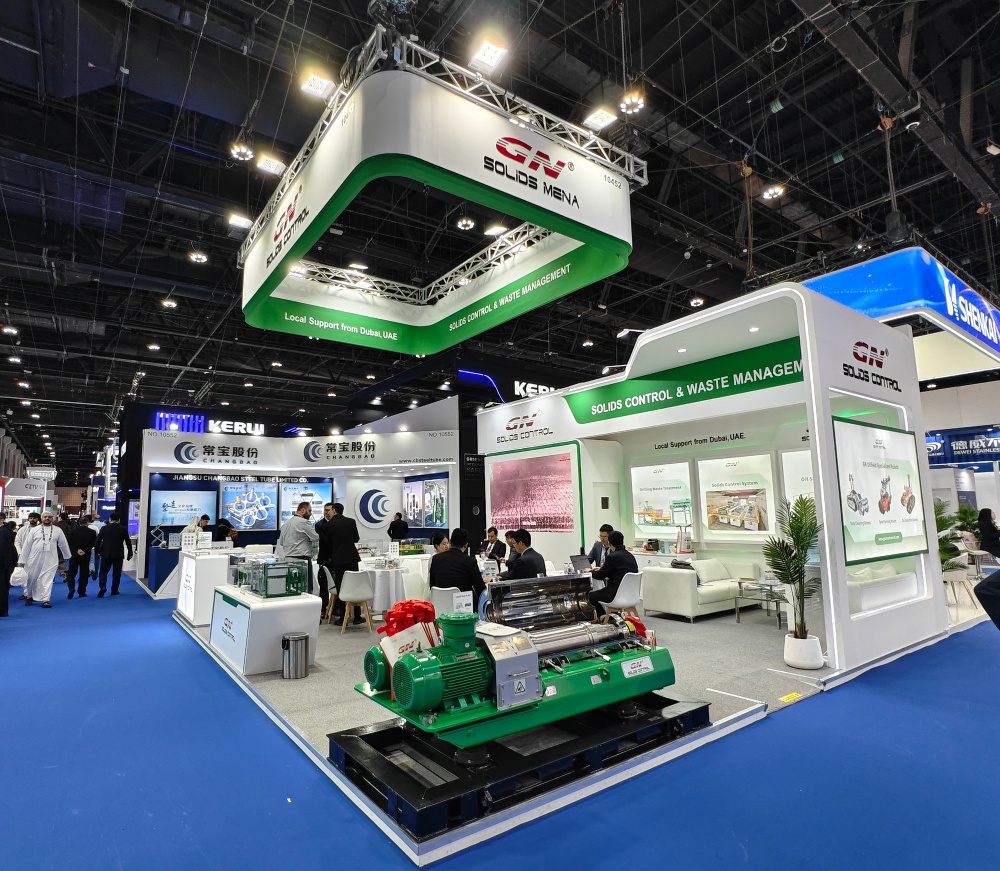
GN Solids Control successfully participated in **ADIPEC 2026**, held from November 2 to 5 at the Abu Dhabi National Exhibition Centre (ADNEC), Abu Dhabi, UAE. As one of the world’s leading energy industry exhibitions, ADIPEC provided an excellent platform for GN to connect with industry professionals, meet existing business partners and explore new opportunities in the global oil and gas market.

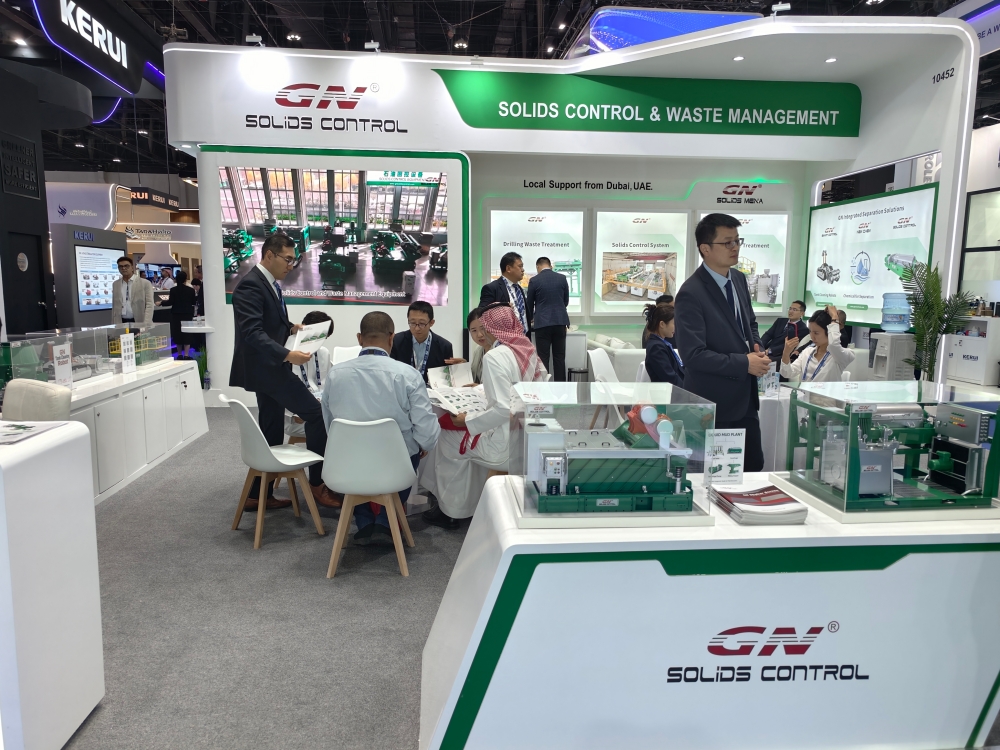
During the four-day exhibition, GN welcomed visitors and customers at **Booth 10452, Hall 10**, where the company presented its comprehensive solids control and drilling waste management solutions. The exhibition attracted professionals from various sectors, including drilling contractors, oilfield service companies, equipment distributors and engineering companies.

Showcasing Integrated Solids Control Solutions
GN Solids Control has extensive experience in designing and manufacturing equipment for drilling fluid processing and solids control applications. Its product portfolio covers shale shakers, mud cleaners, desanders, desilters, decanter centrifuges, vacuum degassers, mud tanks and complete solids control systems.

At ADIPEC 2026, GN focused on communicating its engineering capabilities and integrated solutions for different drilling environments. From individual equipment supply to customized solids control systems and drilling waste management packages, GN aims to help customers improve operational efficiency, reduce waste handling costs and achieve more effective drilling fluid management.

Building Stronger Connections in the Middle East
One of the highlights of ADIPEC 2026 was the opportunity to meet customers and partners from across the Middle East and other international markets. Face-to-face discussions enabled GN to better understand customers’ project requirements, technical challenges and expectations for equipment performance and after-sales support.

Several productive meetings were held during the exhibition, identifying potential cooperation opportunities and establishing clear directions for further discussions and project follow-ups.

GN also continues to strengthen its regional presence through **GN Solids MENA Trading FZE**, its Dubai-based operation in Jebel Ali. With dedicated sales, technical and service teams, GN Solids MENA is positioned to provide more responsive local support, facilitate communication and improve service accessibility for customers throughout the Middle East.

Looking Ahead: Long-Term Cooperation and Local Support
Following GN’s participation in ADIPEC 2026, the company will continue following up with customers and partners, translating exhibition discussions into practical projects and long-term business cooperation.

With manufacturing expertise in China and growing regional support capabilities in the UAE, GN Solids Control remains committed to delivering reliable equipment, customized engineering solutions and professional technical support to the global drilling industry.

Thank you to everyone who visited GN at ADIPEC 2026. We look forward to turning new connections into successful partnerships and working together on future projects!
GN Solids Control | Your Reliable Partner in Solids Control and Drilling Waste Management.

2 Sets GNMS-1000GPM Trailer Mounted Mud Recycling System for Middle East HDD Company

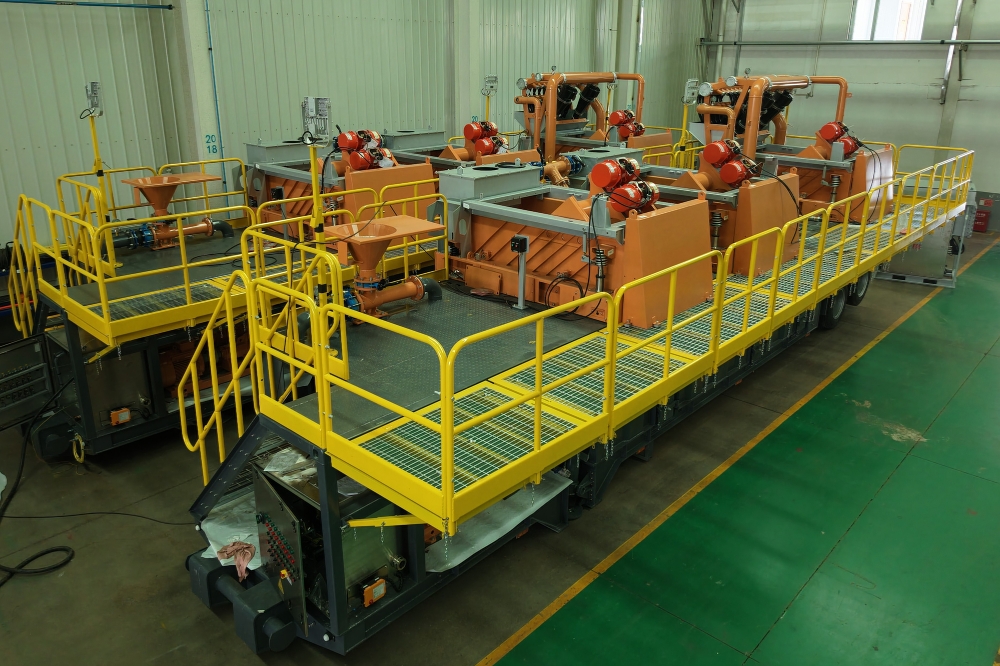
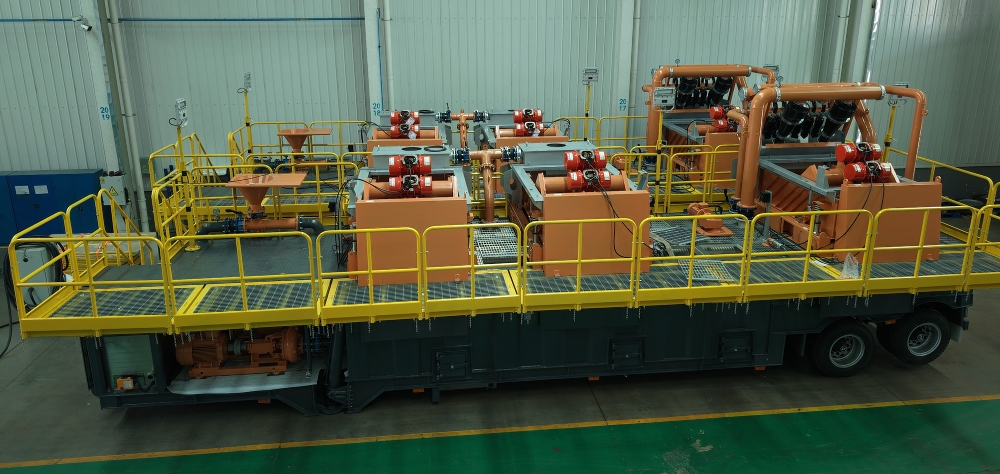
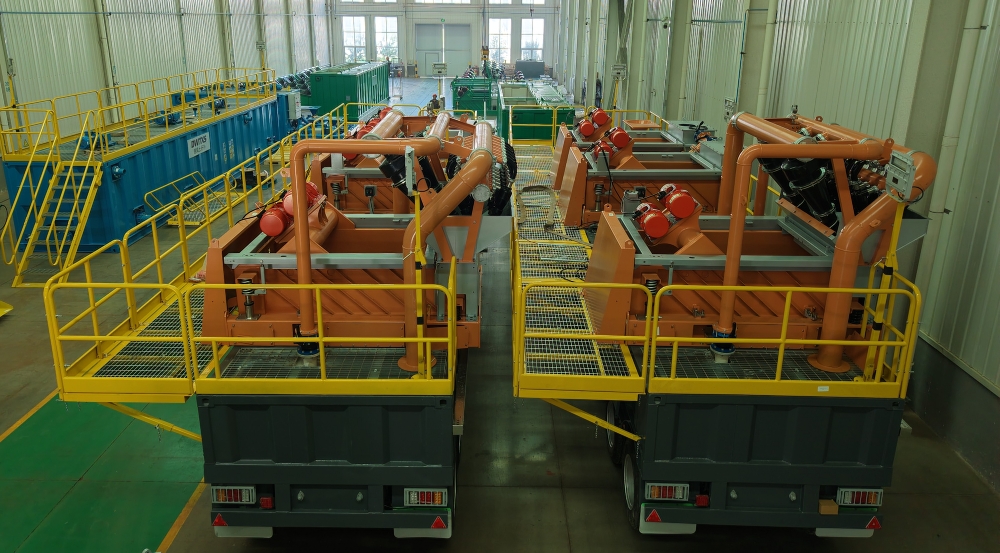
GN Solids Control is supplying 2 sets of GNMS-1000GPM Trailer Mounted Mud Recycling Systems for a Middle East HDD (Horizontal Directional Drilling) company, providing an integrated solution for drilling fluid cleaning, recycling and mixing. Designed for demanding HDD applications, these systems combine mobility, practical equipment integration and reliable solids control technology to support efficient field operations.

Integrated Mud Recycling for HDD Projects
In HDD construction, drilling fluid plays a vital role in borehole stability, cuttings transport, lubrication and cooling. Effective mud recycling helps reduce drilling fluid consumption, manage waste generation and maintain consistent drilling performance.

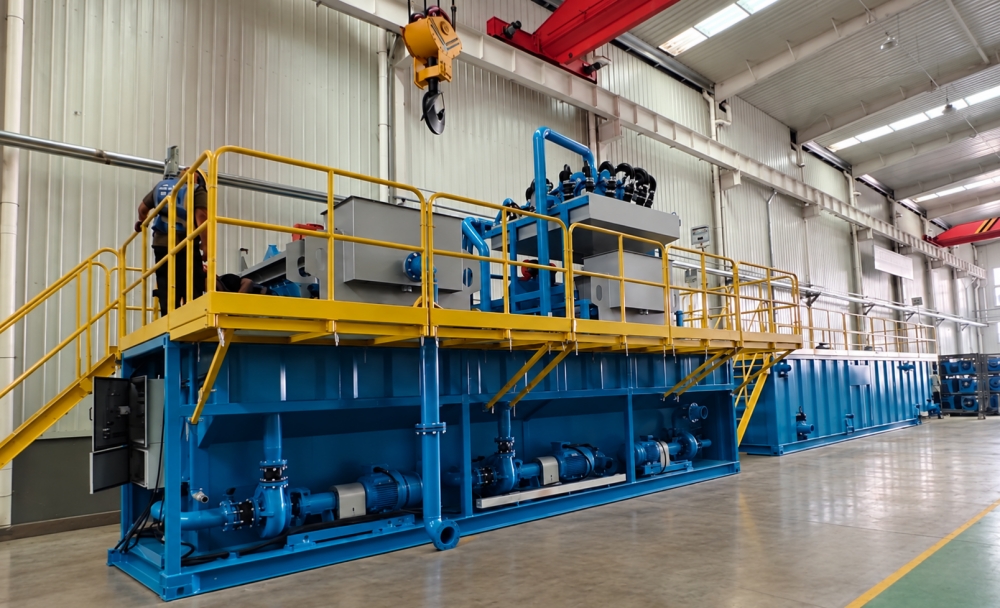
Each system is designed around a trailer-mounted mud tank measuring approximately 13,393 × 2,400 × 2,100 mm, with three internal compartments to support different stages of mud handling and storage. Hydraulic landing legs provide additional support during site operation, while the integrated trailer configuration offers practical transportation and deployment advantages.

Multi-Stage Solids Control Performance
The equipment package incorporates GN shale shakers, mud cleaners and centrifugal sand pumps to establish a multi-stage solids separation process.

The GNZS594K shale shakers provide primary screening to remove larger drilled solids from returning drilling fluid. The GNZJ594K-2S12N mud cleaners, combining desander and desilter hydrocyclones with fine screening, support further removal of finer solids.

GNSB6×5C-12J centrifugal sand pumps supply drilling fluid to the separation equipment, with dedicated pumps also included for mixing operations. A GNSLDSC mixing hopper and GNJBQ075GD mud agitator help facilitate drilling fluid preparation and conditioning.

For additional fluid transfer requirements, the package also includes submersible slurry pumps with supporting frames and dedicated control arrangements.

Designed for Practical Field Operation
Beyond the core separation equipment, the systems incorporate walkways, handrails, ladders, unions and flexible connections to support equipment access and installation.

The electrical control system is designed for 380V/50Hz service, with coordinated equipment controls, phase-sequence protection and wireless remote operation for designated pumps and the agitator. Convenient electrical connections help simplify equipment disassembly and maintenance.

The project also includes screen assemblies and spare screening components to support ongoing operation and maintenance.

Supporting Efficient HDD Construction
With two integrated mud recycling systems, GN Solids Control helps HDD contractors establish a more organized drilling fluid management process across their projects.

By combining solids separation, mud storage, mixing and fluid transfer within a practical mobile solution, the GNMS-1000GPM system is designed to help contractors improve operational flexibility and drilling fluid reuse.

GN Solids Control continues to provide engineered solids control and mud recycling solutions for HDD, trenchless construction and other demanding drilling applications worldwide.

Five GN Decanter Centrifuges Successfully Commissioned for an Overseas Mine Tailings Slurry Separation Project

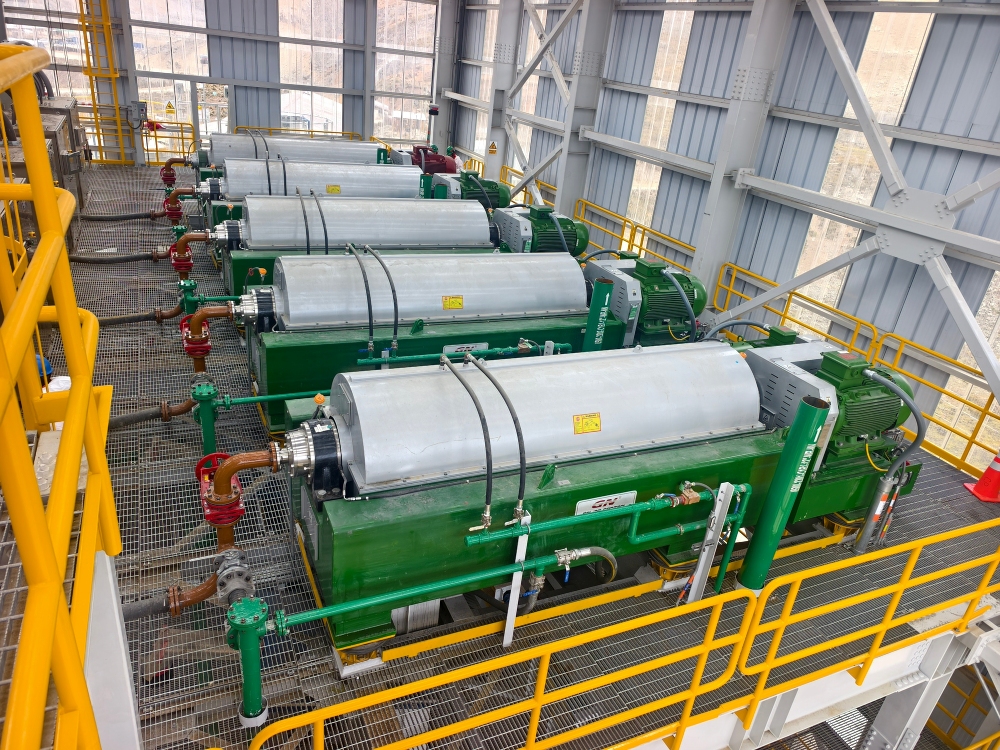
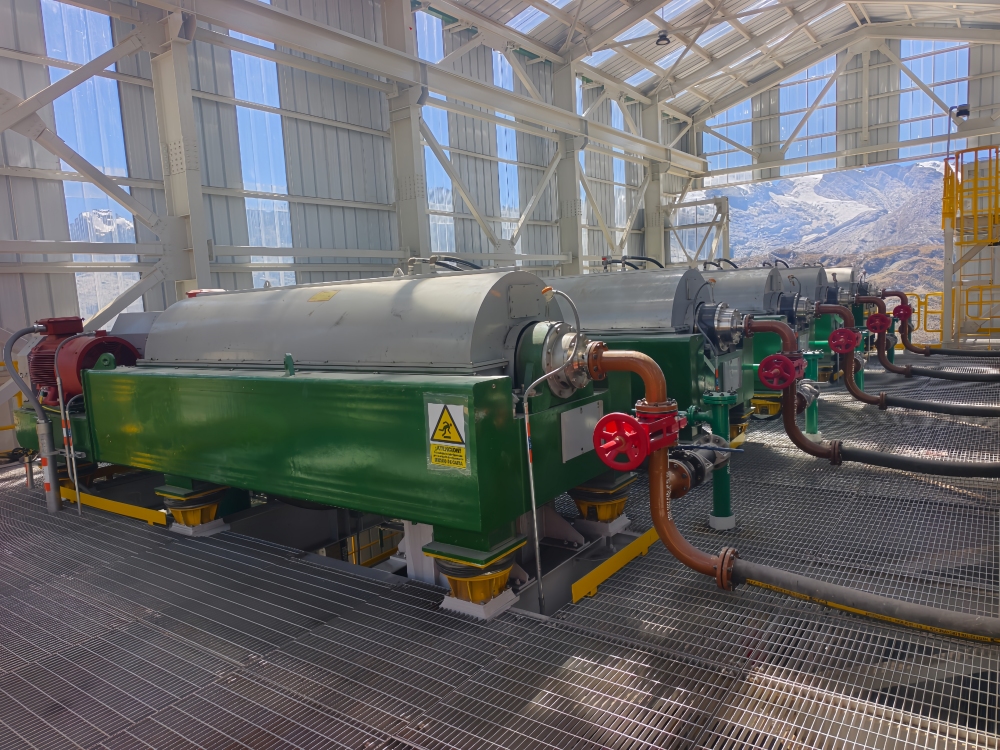
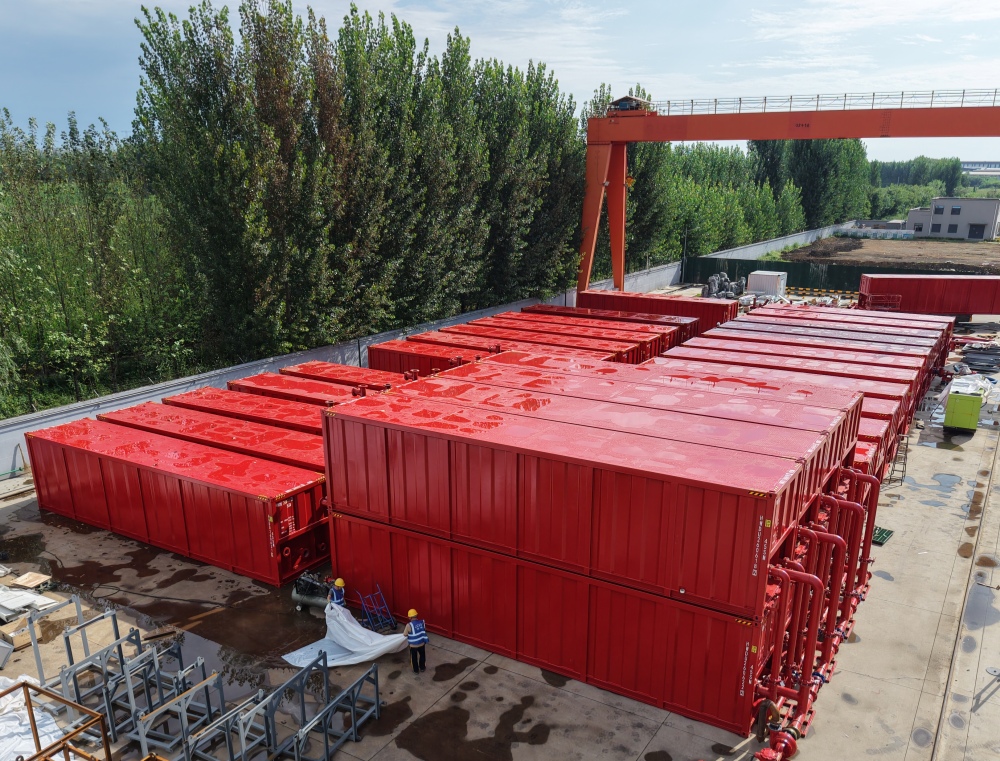
From successful field testing to full-scale commissioning, GN Solids Control has achieved another milestone in the global mining industry. Five GN GNLW764-VFD variable-frequency decanter centrifuges have been successfully commissioned and are now operating reliably at a major overseas mine tailings slurry separation project.

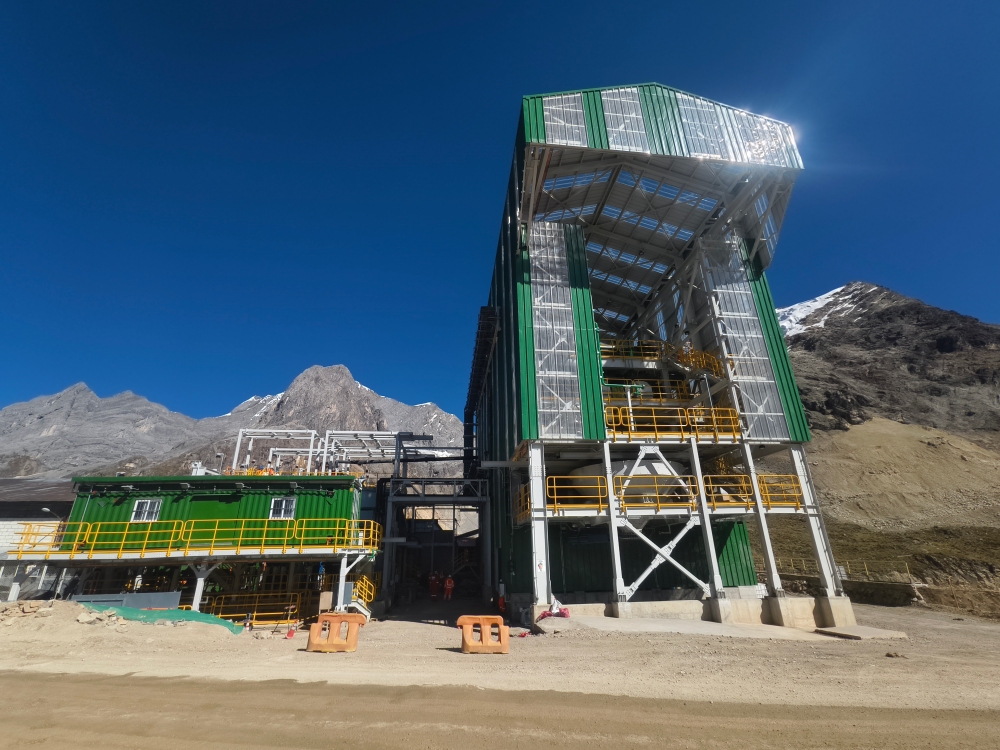
Located at an altitude of approximately 4,500 meters above sea level, the mine presents exceptional challenges for separation equipment. High-altitude conditions, large slurry volumes, hard mineral particles, and severe abrasive wear all demand reliable equipment design and consistent separation performance.

Proven Performance Earns Customer Confidence
The project was awarded through a highly competitive international tender with stringent technical and qualification requirements. To demonstrate equipment performance under actual operating conditions, GN initially supplied one GNLW764-VFD decanter centrifuge for field testing.

During an extended period of operation, the pilot unit demonstrated stable performance, satisfactory separation results, energy-efficient operation, and a low incidence of equipment failures, according to project feedback.

Impressed by the field results, the customer subsequently placed an additional order for four identical centrifuges, bringing the total project quantity to five units.

This step-by-step cooperation reflects the value of real-world equipment validation in demanding mining applications.
Engineered for High-Capacity Tailings Treatment
The GN GNLW764-VFD features a 30-inch-diameter centrifuge bowl and a variable-frequency drive system, allowing operating parameters to be adjusted according to slurry characteristics and process requirements.

For highly abrasive mineral slurry, wear resistance is particularly important. GN incorporates optimized material selection and wear-resistant design enhancements to help extend component service life and support continuous operation.

The variable-frequency configuration also offers operational flexibility, helping the customer balance separation performance, throughput, and energy consumption.

An Integrated Separation Solution
Beyond the five decanter centrifuges, the supplied system includes a 6,000-liter automatic chemical dosing unit and dedicated screw pumps, forming an integrated tailings slurry treatment solution.

The coordinated system supports chemical conditioning, controlled slurry feeding, and continuous solid-liquid separation. By efficiently separating liquid and solids, it helps improve tailings management, facilitate water recovery, and support the customer’s environmental treatment objectives.

Advancing Mining Separation Technology
From international tender qualification to pilot testing and successful commissioning, this project demonstrates GN Solids Control‘s engineering capabilities, customization expertise, and commitment to reliable equipment performance.

GN will continue to provide practical, high-performance separation solutions that help mining operators improve productivity, manage operating costs, and advance more sustainable mineral processing operations.

GN Solids Control showcases mud treatment systems for trenchless construction!

The global trenchless construction industry continues to advance, driven by the demand for efficient underground infrastructure development, reduced surface disruption, and more sustainable construction practices. From urban pipeline installation to large-scale tunnel excavation, effective mud recycling and slurry separation are essential for maintaining stable operations and controlling project costs.

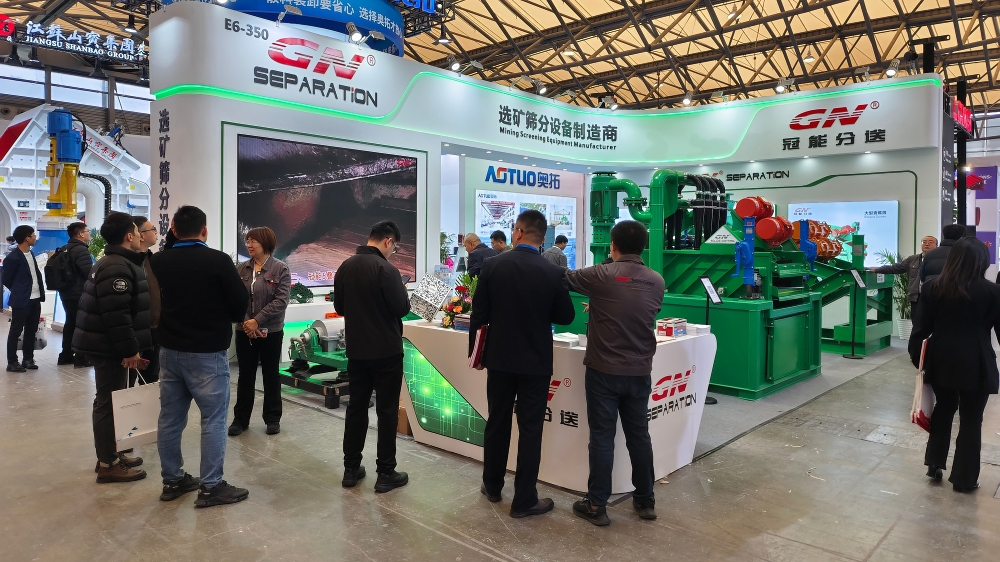
GN Solids Control invites industry professionals, engineering contractors, and business partners to connect with us at bauma CHINA 2026!
Date: November 24–27, 2026
Venue: Shanghai New International Expo Centre (SNIEC), Pudong, Shanghai, China
For official exhibition information, please visit the bauma CHINA website. The New International Expo Centre exhibition dates are confirmed as November 24–27, 2026.

Comprehensive Mud Treatment Solutions for Trenchless Projects
GN Solids Control specializes in solid-liquid separation technologies and provides mud treatment solutions for a wide range of trenchless construction applications. At the exhibition, we look forward to discussing how our equipment can support contractors working on HDD, TBM, and other underground engineering projects.
HDD Mud Recycling Systems
Horizontal Directional Drilling requires effective drilling fluid management to transport cuttings, support borehole stability, and maintain drilling efficiency. GN HDD mud recycling systems can integrate shale shakers, desanders, desilters, centrifugal pumps, and mud tanks according to project requirements.
By removing drilled solids and recovering reusable drilling fluid, these systems help reduce bentonite consumption, minimize waste generation, and improve overall operational efficiency.

TBM Slurry Separation Systems
For tunnel boring projects, high-volume slurry treatment is critical to continuous excavation. GN TBM slurry separation systems use multi-stage separation processes to remove coarse and fine particles from excavated slurry.
Depending on the required capacity and geological conditions, system configurations can incorporate screening equipment, hydrocyclones, pumps, storage tanks, and other supporting components. The objective is to recover reusable water or slurry while improving the management of separated solids.

Meet GN at bauma CHINA 2026
Every trenchless project presents different challenges, from varying soil conditions and slurry characteristics to limited installation space and demanding transportation requirements. GN focuses on providing practical, project-oriented equipment configurations to meet these needs.
Whether you are planning an HDD pipeline crossing, a municipal utility installation, or a large TBM tunneling project, our team welcomes the opportunity to discuss your technical requirements and explore potential cooperation.

Join us in Shanghai from November 24 to 27, 2026, at the Shanghai New International Expo Centre!
Let’s exchange ideas, explore new opportunities, and work together toward more efficient trenchless construction.

GN Solids Control: Your Partner in Mud Recycling and Slurry Separation Solutions.

GN Trenchless Mud Recycling Systems for Overseas Engineering Company

For international engineering companies, trenchless projects rarely follow exactly the same operating pattern. An HDD crossing may require a compact and mobile mud recycling system, while a large TBM project can demand high-capacity slurry separation running continuously throughout excavation. Different equipment, geology, slurry characteristics, and site layouts all require a carefully engineered separation solution.

To support an overseas engineering company with its growing trenchless construction activities, GN Solids Control supplied multiple sets of mud treatment systems covering both HDD mud recycling and TBM slurry separation applications. The project highlights the importance of matching separation technology with the specific requirements of each underground engineering operation.

Solutions Built Around the Project
For HDD operations, the drilling fluid is continuously circulated through the borehole to transport cuttings back to the surface. As solids accumulate, the mud properties can change and drilling performance may be affected.

GN HDD mud recycling systems are configured to remove drilled solids while recovering usable drilling fluid. Depending on capacity and geological conditions, the system can integrate shale shakers, hydrocyclones, centrifugal pumps, mixing equipment, and mud tanks.

The treated mud can then be returned to the drilling operation, helping reduce bentonite consumption and the amount of waste requiring disposal.

High-Capacity Separation for TBM Projects
TBM excavation presents a different challenge. Large quantities of slurry containing excavated soil and fine particles can be generated continuously. The separation system must therefore maintain stable processing capacity while producing a suitable slurry or water stream for reuse.

GN TBM slurry separation systems utilize multi-stage separation technology, combining screening and hydrocyclone-based separation with other equipment according to project requirements. Coarse and fine particles are progressively removed, allowing the treated slurry or water to be circulated back into the TBM system.

Supporting Multiple Projects with One Technology Partner
For engineering companies working across different countries and project types, equipment flexibility can be just as important as separation performance. GN systems can be configured according to required capacity, separation stages, footprint, transportation conditions, and site layout.

Modular system design also helps simplify transportation and installation, particularly for projects where equipment must be mobilized to remote or rapidly developing construction sites.

By supplying both HDD mud recycling systems and TBM slurry separation systems, GN provides engineering contractors with a broader range of trenchless separation solutions under one technology platform.

From drilling fluid recovery to excavated slurry treatment, GN Solids Control continues to support international underground construction projects with practical, efficient, and project-oriented separation technology.

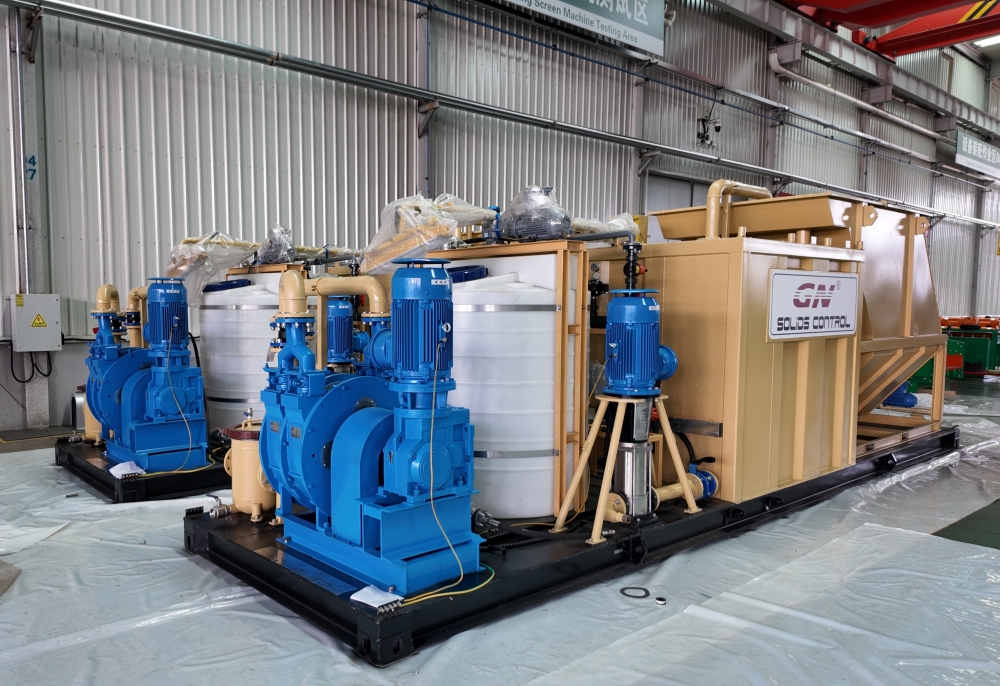
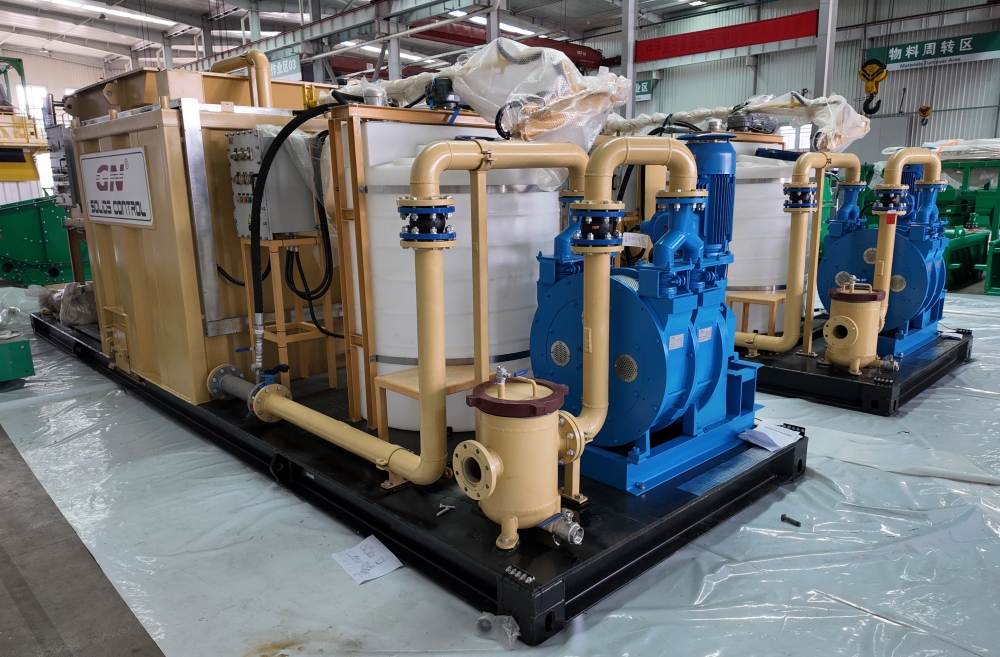
Four Sets Drilling Mud Tank Cleaning Waste Water Treatment Unit for Africa

As drilling activities continue to expand across Africa, efficient wastewater and waste management has become increasingly important for drilling contractors and oilfield service companies. During drilling mud tank cleaning, a considerable amount of wastewater containing residual drilling fluids, fine solids, oil-based contaminants, and suspended particles can be generated. Proper treatment is essential to reduce waste volume, recover reusable water, and meet environmental requirements.

GN Solids Control recently supplied four sets of drilling mud tank cleaning wastewater treatment units for an African project, providing the customer with a practical and efficient solution for handling wastewater generated during mud tank cleaning operations.

Efficient Treatment of Complex Wastewater
Wastewater from drilling mud tank cleaning can have a highly variable composition. It may contain fine drilling solids, residual mud, polymers, weighting materials, and other contaminants. Simply discharging this wastewater is not an efficient or environmentally responsible option.

GN’s treatment system is designed to combine solid-liquid separation and wastewater conditioning processes. Depending on the actual wastewater characteristics, the system can utilize screening, centrifugal separation, chemical dosing, and other treatment stages to progressively remove suspended and fine solids.

The separated solids can be collected for further treatment or disposal, while the clarified liquid can be recovered for reuse or transferred to subsequent treatment processes.

Compact Design for African Projects
For projects in Africa, transportation, installation, and site conditions are often important considerations. GN therefore focuses on practical system design, with compact equipment layouts and modular configurations that simplify transportation and installation at remote drilling sites.

The four supplied units allow the customer to establish multiple treatment points or deploy the systems according to different drilling operations, improving flexibility and operational efficiency.

Supporting More Sustainable Drilling Operations
Effective wastewater treatment can reduce the volume of liquid waste requiring disposal while maximizing water recovery. At the same time, improved solids removal helps protect downstream equipment and makes subsequent treatment processes more efficient.

With extensive experience in drilling fluids solids control, wastewater treatment, and drilling waste management, GN Solids Control provides customized separation solutions for oilfield projects worldwide.

From individual equipment to complete treatment systems, GN is committed to helping drilling contractors improve waste management efficiency, resource recovery, and environmental performance in challenging operating environments.

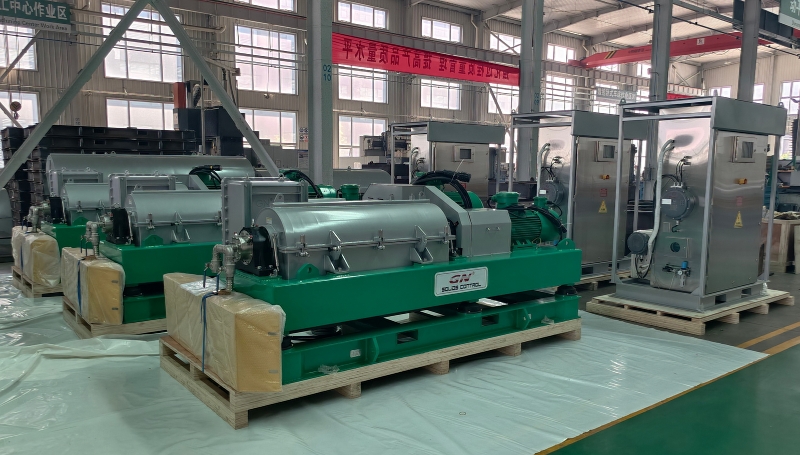
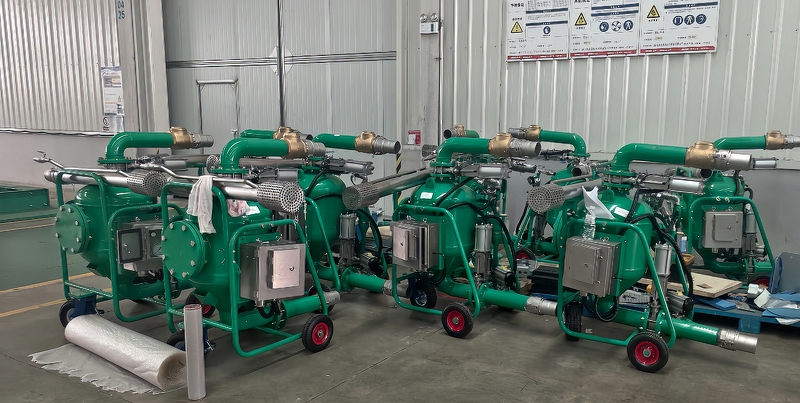
GN Solids Vauum Pump and Decanter Centrifuge for Middle East Client

In modern drilling and oilfield waste management, efficient fluid transfer and reliable solids separation are essential for maintaining stable operations. For customers working in the demanding Middle East market, equipment must deliver dependable performance while handling challenging operating conditions. Recently, GN Solids Control supplied a Vacuum Pump and Decanter Centrifuge package to a Middle East client, providing complementary technologies for efficient fluid and solids management.

The combination of a vacuum pump and decanter centrifuge creates an effective solution for handling drilling fluids, sludge, and other challenging liquid-solid mixtures. While the vacuum pump focuses on efficient material transfer, the decanter centrifuge performs continuous mechanical separation, allowing the two technologies to work together within an integrated treatment process.

Efficient Vacuum Transfer
GN’s Vacuum Pump is designed for efficient suction and transfer of fluids and sludge. Compared with conventional pumping methods, vacuum transfer can provide greater flexibility when handling materials with high viscosity or significant solids content.

The equipment can be used for applications such as tank cleaning, sludge transfer, drilling waste handling, and fluid recovery. By reducing the need for manual handling and improving material transfer efficiency, the vacuum pump helps operators create a cleaner and more controlled working environment.

High-Performance Decanter Centrifuge
Following fluid collection or conditioning, the GN Decanter Centrifuge provides continuous separation of fine solids from liquids.

Using high centrifugal force, the centrifuge separates suspended solids according to their density difference, producing a cleaner liquid phase and a more concentrated solids discharge. This makes the equipment particularly suitable for drilling fluid solids control, sludge treatment, and waste reduction applications.

Effective fine-solids separation can help operators recover valuable drilling fluids, reduce waste volumes, and lower transportation and disposal costs.

Designed for Middle East Operations
The Middle East presents demanding conditions for oilfield equipment, including high ambient temperatures, dusty environments, and intensive continuous-duty operations. GN equipment is engineered with robust structures and carefully selected components to support reliable operation in these environments.

Beyond individual equipment supply, GN can also integrate vacuum pumps, centrifuges, tanks, pumps, and other separation equipment into complete treatment systems according to specific project requirements.

The successful delivery of this package further demonstrates GN’s ability to provide practical separation and waste management solutions for international customers.

From vacuum transfer and sludge handling to high-efficiency centrifuge separation, GN Solids Control continues to help customers improve fluid recovery, reduce waste, and enhance operational efficiency across the global oil and gas industry.

GN Solids 14000BBL Rapid Liquid Mud Plant for Drilling Fluids Company

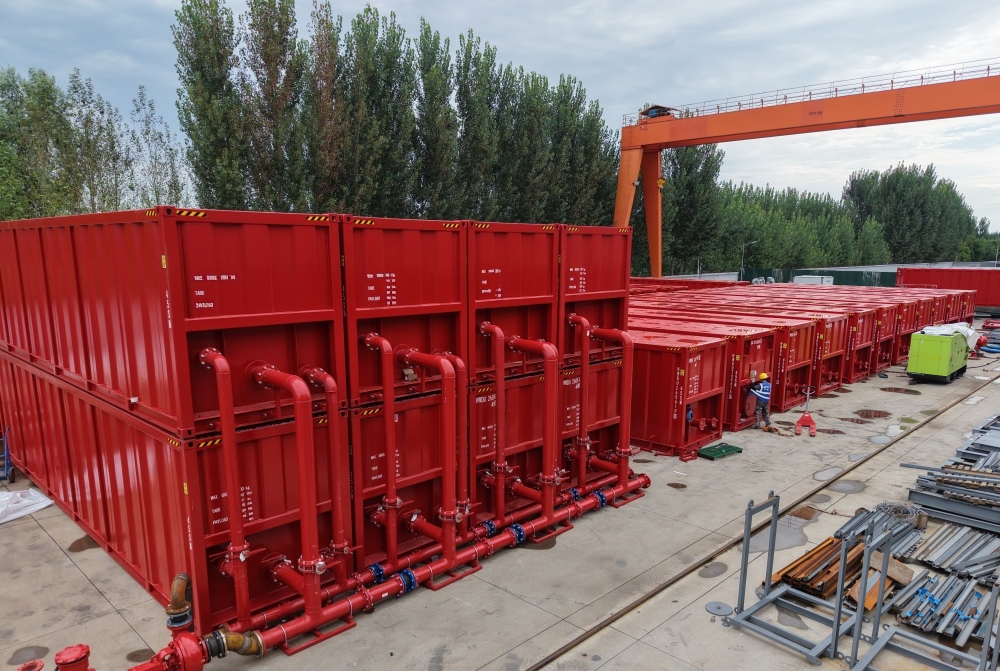
For drilling fluids companies, a large-capacity mud storage system is not simply about how much fluid it can hold. Transportation, installation, site footprint, and future relocation can have a direct impact on project efficiency and operating costs. With this in mind, GN Solids Control has developed a 14,000 BBL Rapid Liquid Mud Plant based on a containerized and modular concept, offering a practical solution for drilling projects that require both high capacity and fast deployment.

One of the key ideas behind this project is transportation efficiency. Traditional mud tanks can be difficult and expensive to transport because of their dimensions. GN’s solution uses tanks designed around a 40-foot High Cube container format, with each tank providing approximately 440 BBL of effective capacity. This standardized configuration makes transportation planning much easier and allows the mud plant to be shipped and relocated using conventional container logistics.

The tanks are also provided with CSC container certification, which is an important feature for international projects. With CSC-certified units, customers have greater flexibility when arranging transportation between countries and project locations. For drilling fluids companies operating across multiple regions, this mobility can provide a significant operational advantage.

Designed According to API-650
Structural reliability is another important consideration. The GN liquid mud tanks are designed according to the API 650 standard, providing an established engineering framework for the design and fabrication of welded storage tanks used in petroleum-related applications.

For a large-capacity mud plant, reliable tank construction is essential because the facility may operate continuously and handle large volumes of drilling fluids. Applying a recognized design standard helps ensure that structural requirements are considered throughout the engineering and manufacturing process.

Making Better Use of Limited Space
A particularly distinctive feature of the GN 14,000 BBL system is its two-level stackable design.

Instead of arranging all tanks horizontally across a large area, the modular tanks can be installed in two levels according to the project layout. This approach can significantly reduce the required ground area while maintaining substantial mud storage capacity.

For drilling sites where land availability is limited, this can make a major difference. A smaller footprint means more efficient site planning and leaves additional space for other drilling fluid equipment, pipelines, access routes, and operational areas.

A Flexible Solution for Changing Projects
The modular design also makes the plant adaptable. Different tank configurations can be arranged according to the customer’s storage requirements, and the system can be relocated or expanded as the drilling campaign develops.

With 440 BBL containerized tanks, CSC certification, API-650 design, and two-level stacking capability, GN’s 14,000 BBL Rapid Liquid Mud Plant combines capacity with mobility and efficient space utilization.

For drilling fluids companies looking beyond traditional mud storage solutions, GN provides a modern approach designed around the realities of international drilling projects: easier transportation, faster deployment, optimized footprint, and dependable storage capacity.

GN Double Deck Shale Shaker for Deep well drilling Projects

Deep well drilling places higher demands on the entire solids control system. As drilling depth increases, operators may face higher circulation rates, heavier drilling fluid, increased solids loading, and longer continuous operating hours. Efficient solids control is therefore essential to maintain drilling fluid performance and support stable drilling operations.

To meet these demanding requirements, GN Solids provides the Double Deck Shale Shaker, designed to deliver high processing capacity and efficient solids separation for challenging drilling projects, including deep well applications.

Higher Capacity with a Compact Footprint
One of the key advantages of a double deck shale shaker is its ability to provide a larger screening area without significantly increasing the equipment footprint.

Compared with a conventional single deck design, the double deck configuration allows multiple screen panels to work simultaneously, increasing the total available screening area and improving the equipment’s solids handling capability. This makes it particularly suitable for projects where high flow rates and large volumes of drilled solids need to be processed continuously.

For drilling rigs with limited space, the double deck design offers an efficient way to increase processing capacity without requiring additional shale shakers or expanding the solids control system.

Flexible Screening for Different Drilling Conditions
Deep well drilling conditions can change significantly as the well progresses. Drilling fluid properties, solids content, and formation characteristics may vary, creating different requirements for solids separation.

The double deck shale shaker provides greater flexibility in screen configuration. Different screen mesh sizes can be selected according to the drilling stage and fluid conditions, helping operators balance processing capacity and separation efficiency.

This flexibility allows the solids control system to adapt more effectively to changing drilling requirements while maintaining stable mud properties.

Supporting Better Drilling Fluid Performance
The shale shaker is the first stage of the solids control process and plays an important role in protecting downstream equipment.

Efficient removal of large drilled solids helps reduce the solids loading on hydrocyclones, mud cleaners, and decanter centrifuges. By reducing unnecessary solids before the drilling fluid reaches downstream equipment, operators can improve overall separation efficiency and reduce equipment wear.

Effective solids removal can also help maintain drilling fluid properties, reduce mud dilution requirements, and lower the consumption of drilling chemicals and replacement fluid.

Reliable Design for Continuous Operation
Deep well drilling projects often require equipment to operate continuously for extended periods. Reliability, maintenance accessibility, and structural strength are therefore important considerations.

GN Double Deck Shale Shakers are designed with a robust structure and efficient vibration system to support continuous solids separation. The equipment can also be customized according to project requirements, including electrical specifications, hazardous-area requirements, screen configuration, and solids control system layout.

With its large screening area, flexible configuration, efficient solids separation, and ability to support demanding drilling operations, the GN Double Deck Shale Shaker provides a practical solution for modern deep well drilling projects.